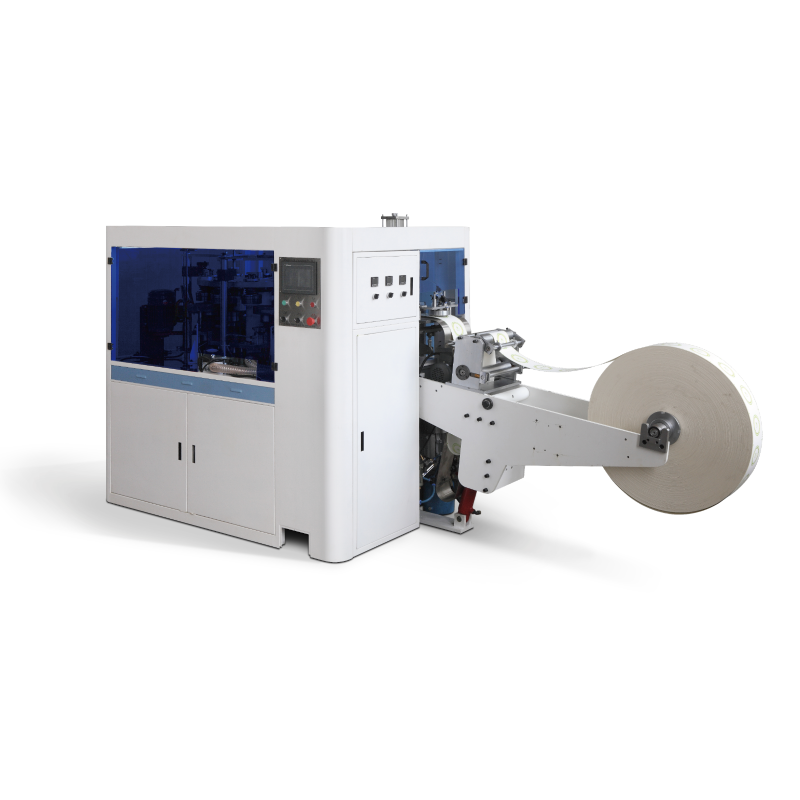
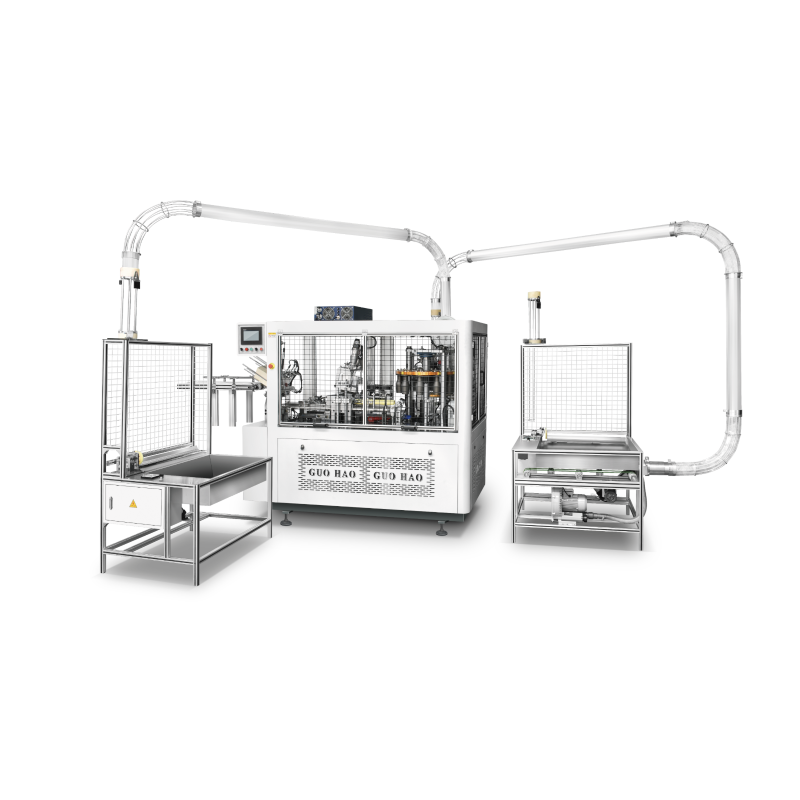
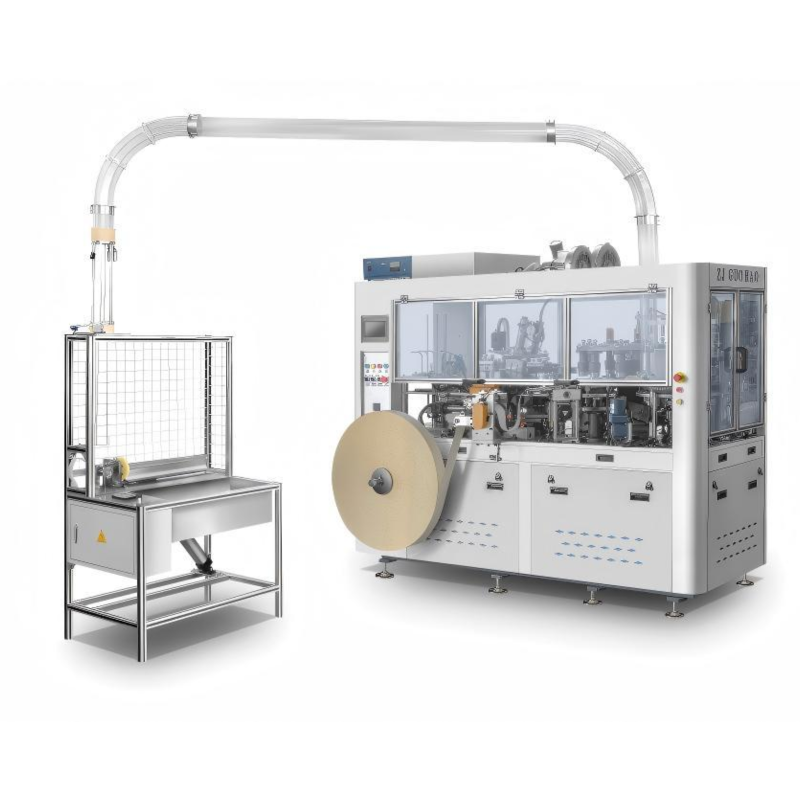
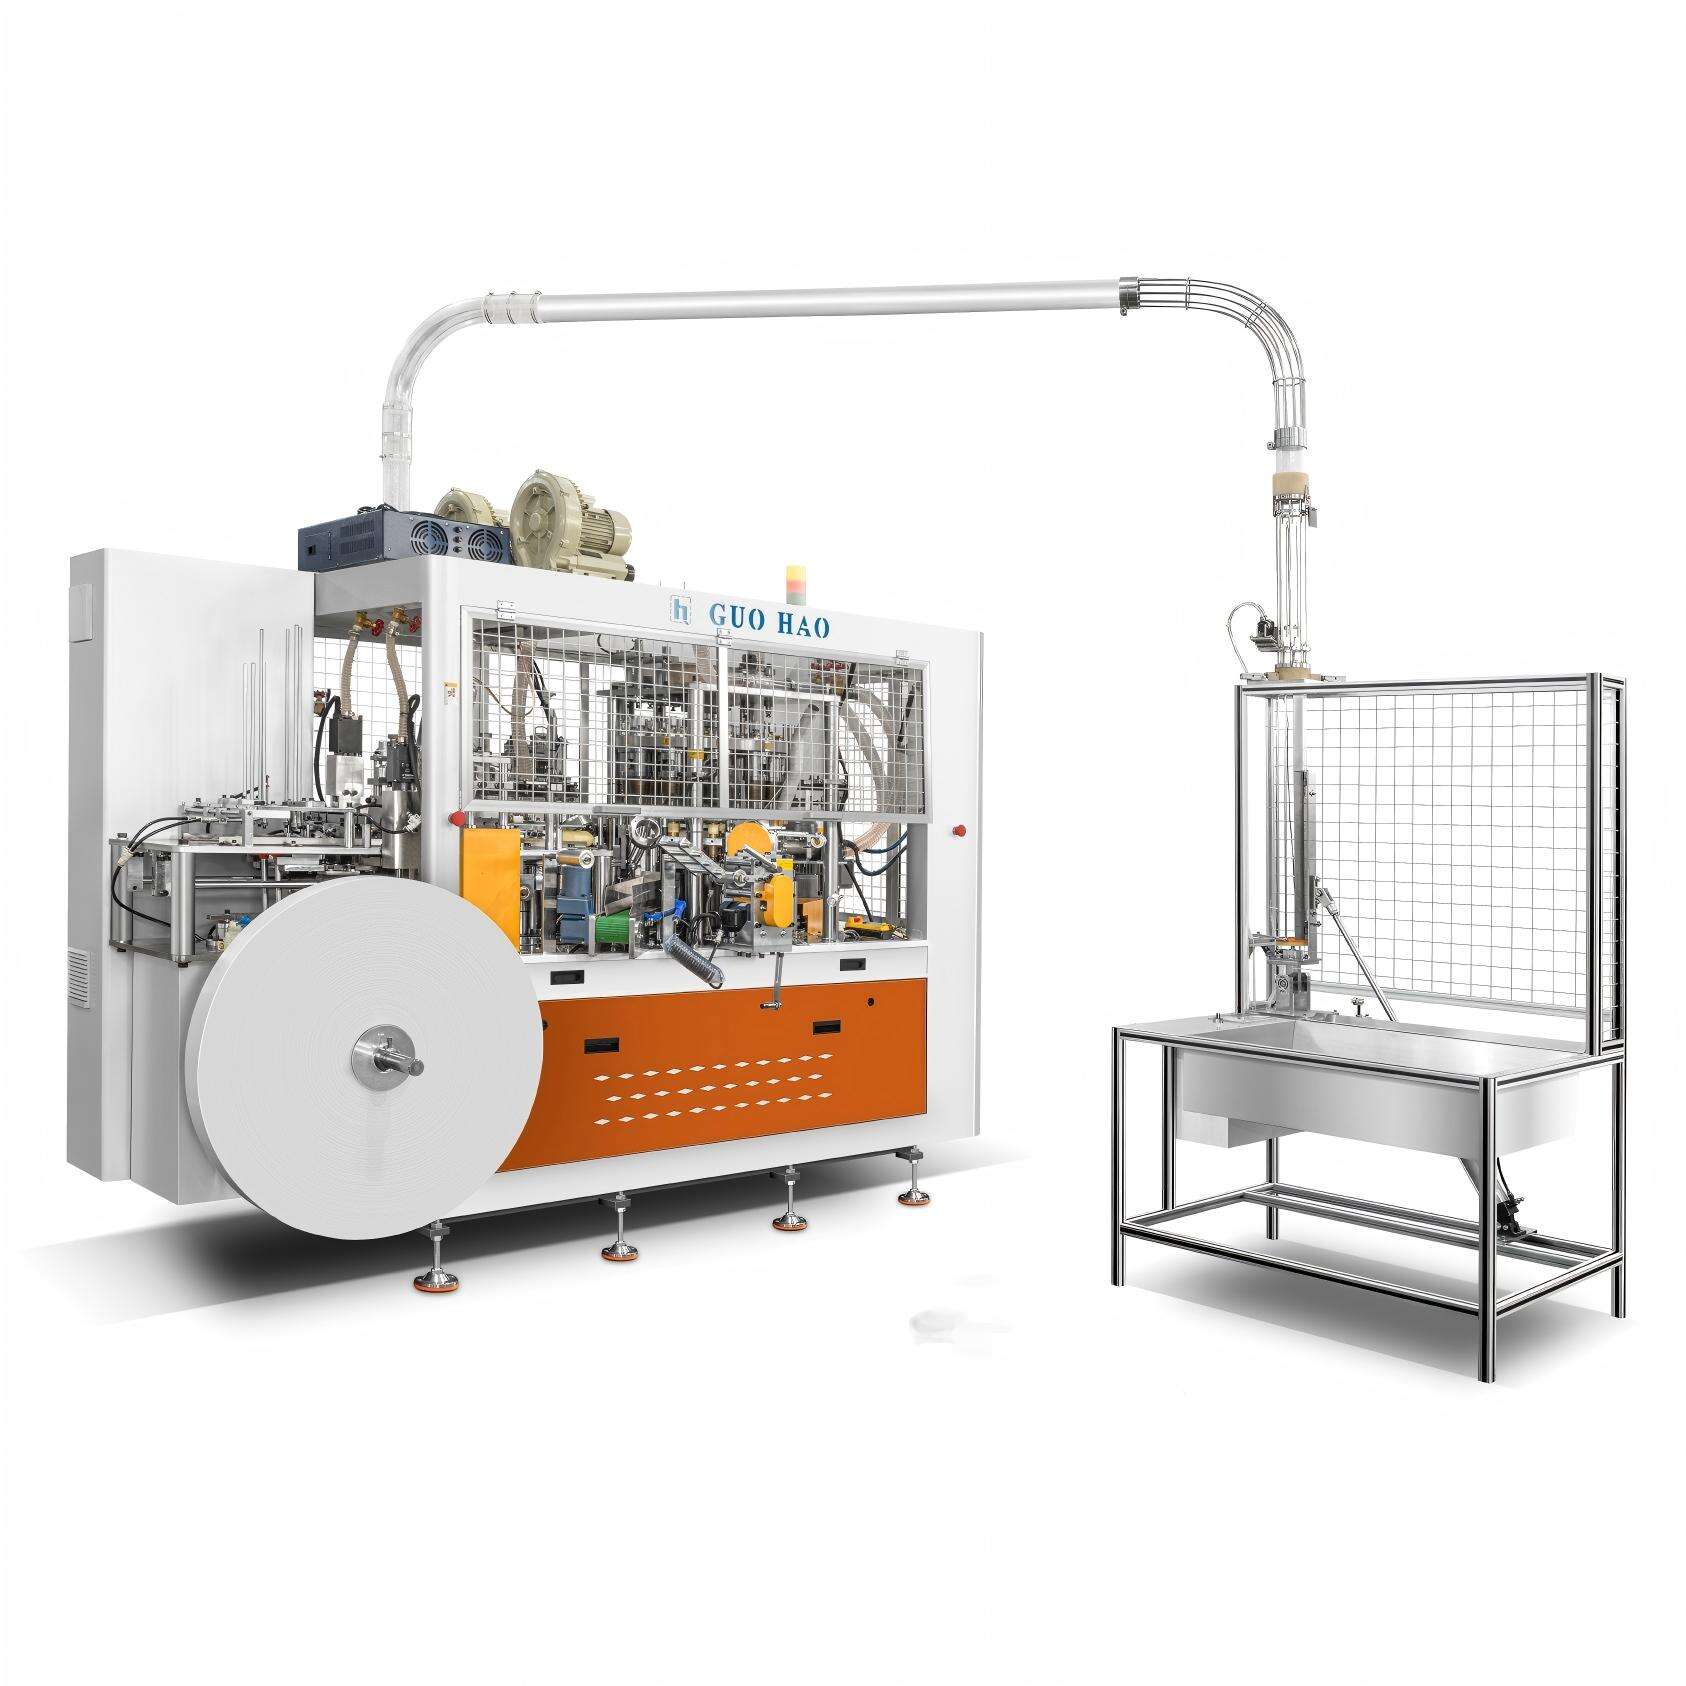
double wall paper cup machine factory
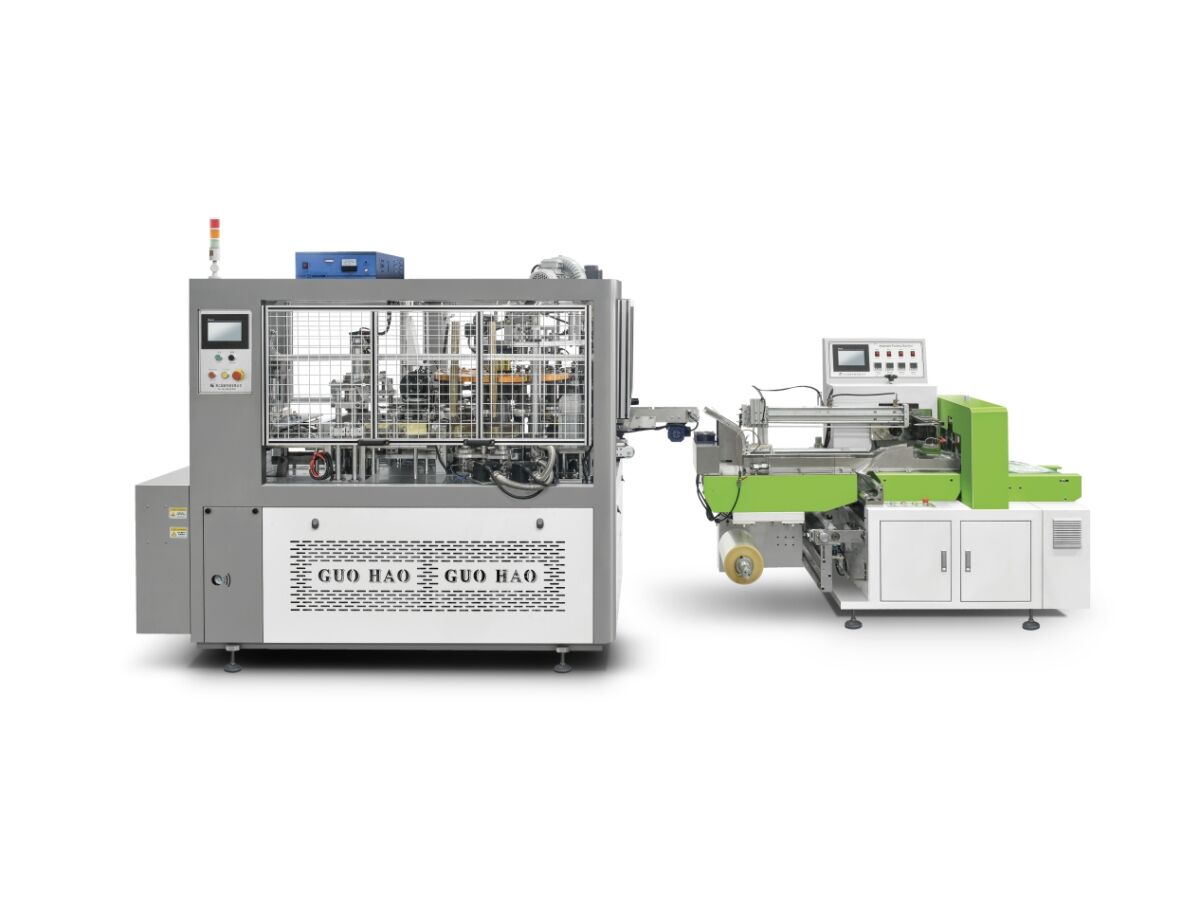
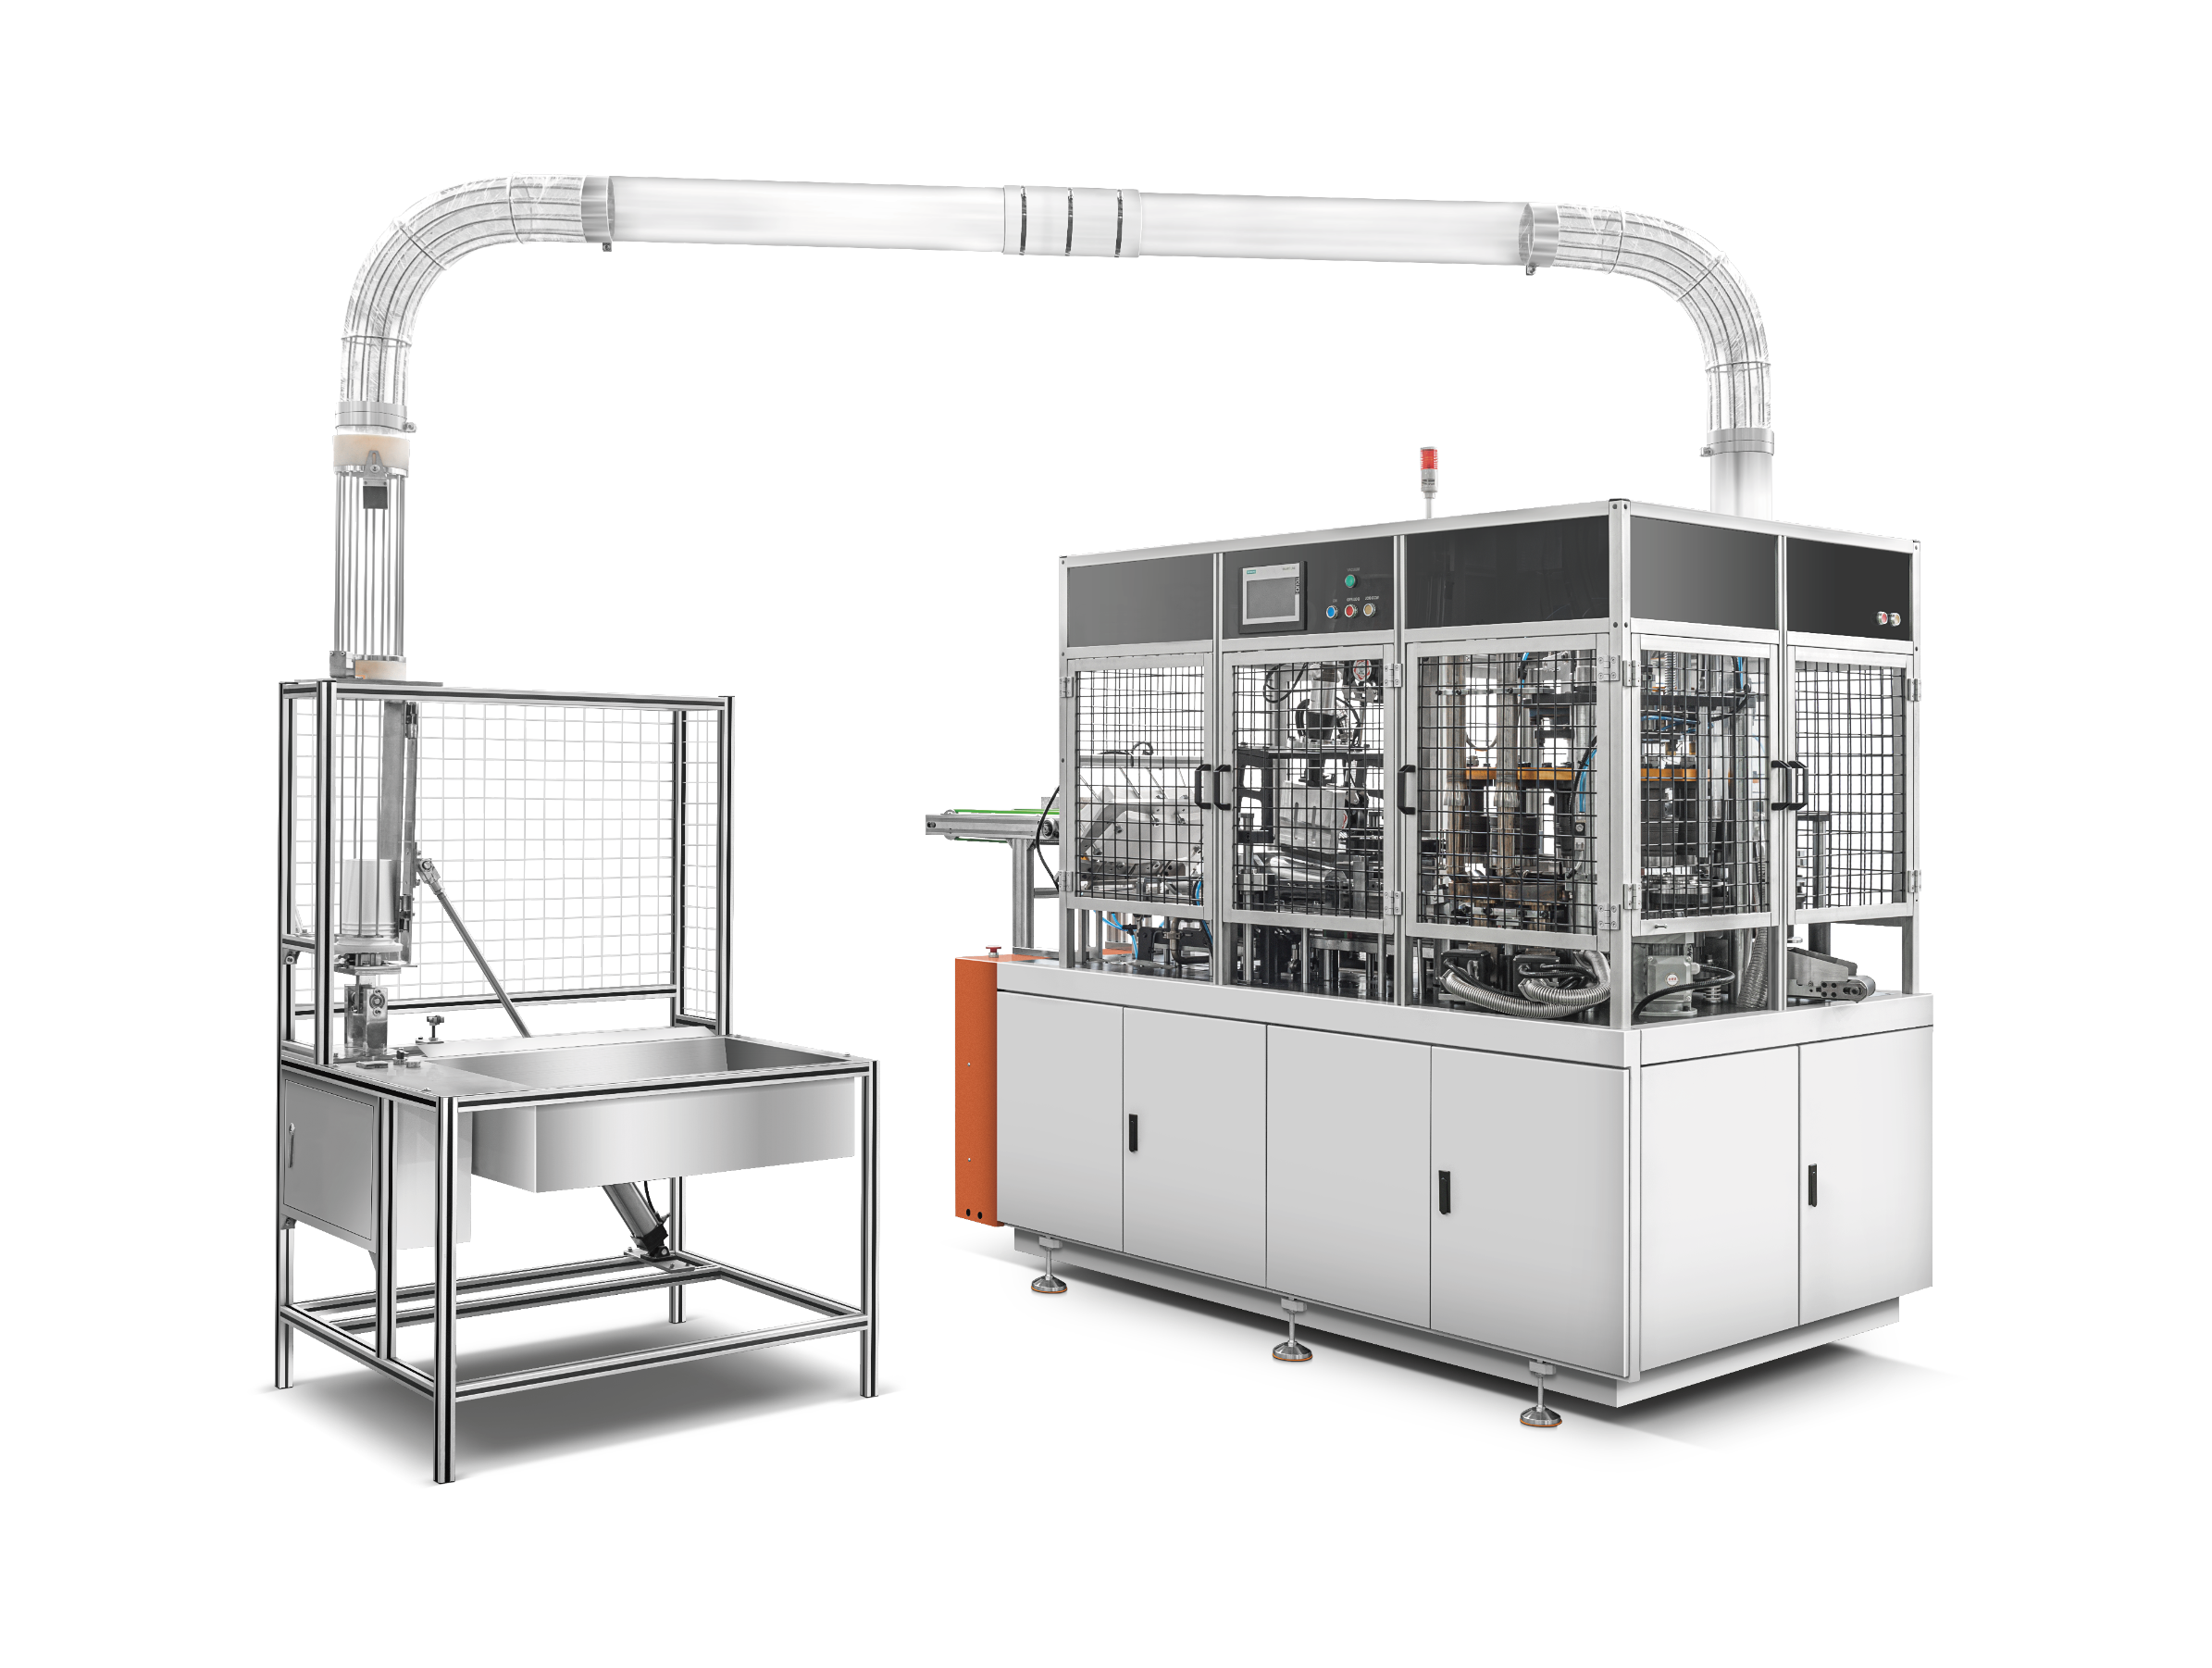
A double wall paper cup machine factory represents a sophisticated manufacturing facility dedicated to producing high-quality insulated beverage containers through advanced automation technology. These specialized production centers house state-of-the-art equipment designed to create double-layered paper cups that provide superior thermal insulation compared to single-wall alternatives. The double wall paper cup machine factory integrates multiple manufacturing processes, including paper feeding, forming, sealing, bottom attachment, and quality control systems, all orchestrated through computerized control panels that ensure consistent product quality and optimal production efficiency. The primary function of a double wall paper cup machine factory revolves around transforming raw paper materials into finished insulated cups through a series of precisely coordinated mechanical operations. The technological features incorporated within these facilities include servo motor control systems that guarantee accurate cup formation, ultrasonic sealing technology that creates leak-proof joints, and automated inspection systems that detect defects during production. Modern double wall paper cup machine factory installations utilize advanced heating elements that maintain optimal temperature conditions throughout the manufacturing process, ensuring proper adhesion between paper layers and creating the characteristic air gap that provides thermal insulation properties. The applications for products manufactured in a double wall paper cup machine factory span across numerous industries, including coffee shops, restaurants, convenience stores, corporate offices, and event catering services. These versatile containers serve hot beverages such as coffee, tea, hot chocolate, and specialty drinks while protecting users from heat transfer and maintaining beverage temperature for extended periods. The double wall paper cup machine factory production output caters to both small-scale local businesses and large commercial operations requiring high-volume cup supplies, with customization options available for branding and sizing requirements to meet diverse market demands.
 ×

 EN